Engineered to mitigate thermal degradation, pump cavitation, and particle wear in heavy machinery.
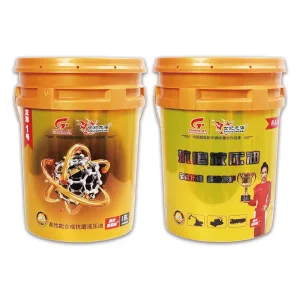
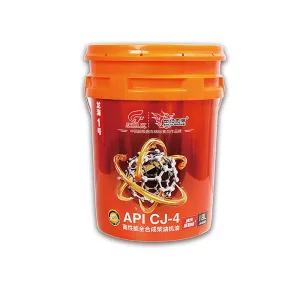
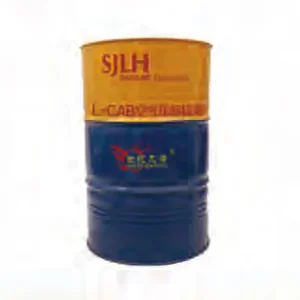
As the commercial capital of Zambia’s Eastern Province and a strategic inland hub bordering Malawi along the Nacala Development Corridor, Chipata is undergoing rapid economic modernization. The city’s industrial ecosystem is anchored by large-scale commercial agriculture (cotton ginning, tobacco processing, corn milling, sunflower oil extraction), municipal infrastructure construction, sub-Saharan regional freight transport, and emerging mineral exploration.
Operating heavy machinery in Chipata presents distinct tribological challenges. Ambient temperatures routinely surpass 35°C during peak dry seasons, causing thermal breakdown, pump oxidation, and varnish accumulation in standard hydraulic fluids. Furthermore, intense airborne particulate loads from unpaved feeder roads and agro-processing operations contaminate system oil, leading to accelerated boundary lubrication failure in high-pressure vane and piston pumps.
As an authoritative Anti-wear Hydraulic Oil Exporter & Exporters for Chipata, Shandong Longhai Lubrication Technology Development Co., Ltd. delivers high-shear-stability hydraulic fluids blended with premium hydrocracked paraffinic base oils and advanced zinc dialkyldithiophosphate (ZDDP) additive systems. Our formulations ensure continuous fluid film integrity, precise hydraulic response, and extended oil drain intervals under Sub-Saharan Africa’s toughest operational environments.
A rigorous examination of molecular chemistry, boundary lubrication mechanisms, and international DIN/ISO compliance.
Our formulation incorporates optimized Zinc Dialkyldithiophosphate chemistry. Under local frictional heating, ZDDP forms a sacrificial polyphosphate protective film over metallic surfaces, preventing metal-to-metal contact inside high-pressure axial piston and vane pumps.
Formulated using severe hydrocracked Group II base stocks, our oils resist thermal decomposition and sludge formation. This eliminates valve sticking, filter clogging, and oil passageway restriction in high-heat sub-Saharan operational environments.
Equipped with specialized surface-active defoamers and rapid demulsifiers, Longhai fluid rapidly separates water ingress (common during humid monsoons in Chipata) and prevents air entrainment, shielding systems against destructive pump cavitation.
| Test Parameter | Test Method | ISO VG 32 | ISO VG 46 | ISO VG 68 | ISO VG 100 |
|---|---|---|---|---|---|
| Kinematic Viscosity @ 40°C (mm²/s) | ASTM D445 | 28.8 – 35.2 | 41.4 – 50.6 | 61.2 – 74.8 | 90.0 – 110.0 |
| Viscosity Index (VI) | ASTM D2270 | ≥ 102 | ≥ 105 | ≥ 100 | ≥ 98 |
| Flash Point (COC) (°C) | ASTM D92 | ≥ 220 | ≥ 230 | ≥ 240 | ≥ 250 |
| Pour Point (°C) | ASTM D97 | ≤ -24 | ≤ -21 | ≤ -18 | ≤ -15 |
| FZG Gear Test (Fail Load Stage) | DIN 51354-2 | > Stage 12 | > Stage 12 | > Stage 12 | > Stage 12 |
| Copper Corrosion (3h @ 100°C) | ASTM D130 | 1a (Pass) | 1a (Pass) | 1a (Pass) | 1a (Pass) |
| OEM Compliance Standards | Global Spec | DIN 51524 Part 2 (HLP), ISO 11158 HM, Parker Denison HF-0/HF-1/HF-2, Eaton Brochure 03-401-2010 | |||
Tailored hydraulic fluid strategies for agricultural processing, heavy civil construction, and logistics operations.
Chipata's large-scale cotton ginning facilities, maize mills, and oilseed pressing plants rely on heavy hydraulic rams, balers, and continuous conveyors. Longhai Anti-Wear Hydraulic Oil ISO VG 46 and 68 provide ultra-clean operation, resisting thermal varnish buildup during long agricultural harvest seasons.
Road maintenance along the Great East Road and local quarrying operations subject excavators, motor graders, and wheel loaders to dusty, high-load conditions. Our high-VI hydraulic oils safeguard axial piston pumps against severe micro-pitting, scuffing, and thermal shearing under continuous shock loading.
As freight flows between Lilongwe and Lusaka through the Chipata border post, heavy transport rigs demand reliable hydraulic steering and power tail-lift systems. Longhai anti-wear fluids guarantee consistent fluid pressure across dynamic temperature transitions from cool nights to hot afternoons.
A global leader in smart lubricant formulation, automated blending, and international export excellence.
Established in 2009 and headquartered in Zibo, Shandong, Shandong Longhai Lubrication Technology Development Co., Ltd. is a high-tech enterprise integrating R&D, production, and sales. Deeply involved in the lubricant industry for over 15 years, Longhai has built a comprehensive industrial chain committed to delivering premium lubrication solutions worldwide.
Longhai Technology owns its proprietary brand "Century Longhai" and strategic cooperation brand British "A Ba" series. The product portfolio encompasses heavy-duty diesel engine oils, gasoline engine oils, gear oils, hydraulic transmission fluids, anti-wear hydraulic oils, engineering machinery fluids, natural gas engine oils, synthetic industrial oils, motorcycle oils, automotive urea solutions, and antifreezes. All brand products are backed by PICC China People's Insurance Company quality coverage.
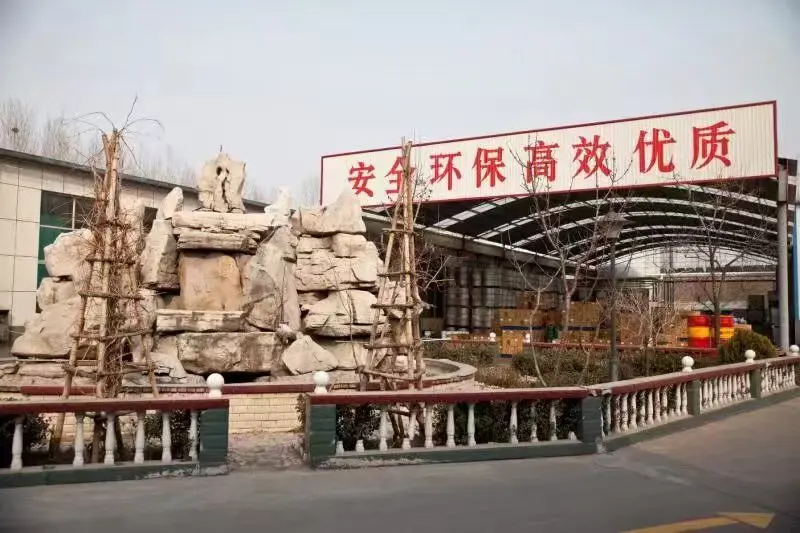
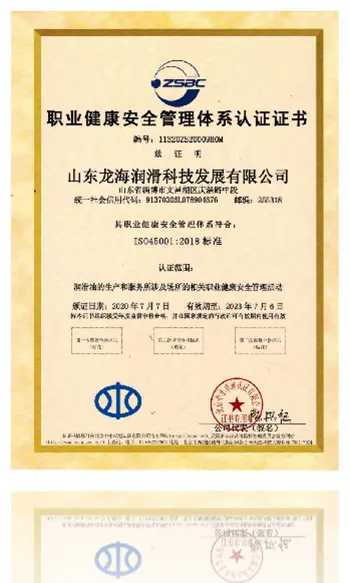
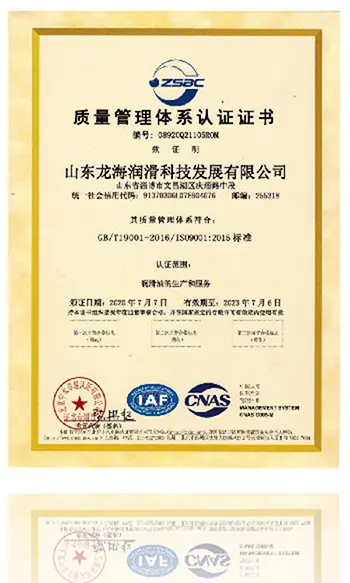
Shandong Longhai strictly adheres to international manufacturing standards. The company has certified compliance with ISO 9001:2015 Quality Management Systems, ISO 14001:2015 Environmental Management Systems, and ISO 45001:2018 Occupational Health and Safety Management Systems. Furthermore, our fluid technologies hold prestigious OEM approvals, including Automatic Transmission Mercedes-Benz Certification, providing absolute quality assurance for Chipata commercial buyers.
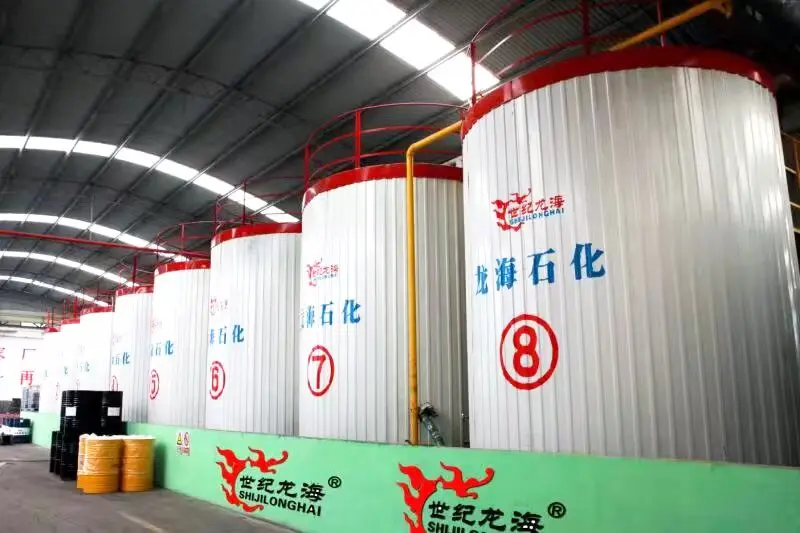
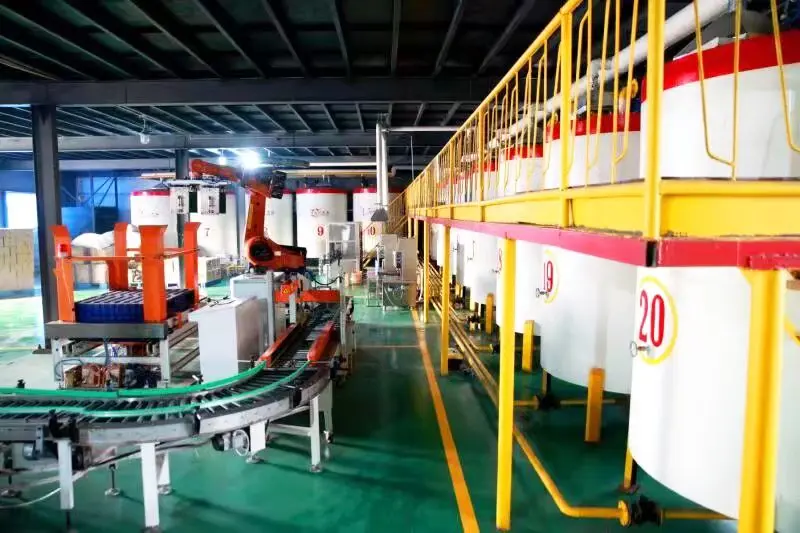
Longhai Technology operates a state-of-the-art production base spanning 131 acres, achieving an annual manufacturing capacity of 200,000 tons. Our facility is equipped with automated high-precision blending kettles and high-speed metering filling lines that achieve filling accuracies within 1‰ to 2‰, while boosting operational speeds by 20% to 35% over traditional systems.
Reinvesting over 5% of annual revenue into R&D, Longhai collaborates with leading universities and research institutes. Our sales network covers 139 cities across 29 domestic provinces and exports to dozens of international markets in Sub-Saharan Africa, Southeast Asia, and Central Asia.
End-to-end private labeling, custom formulation engineering, and resilient export logistics.
Engineered anti-wear and synthetic hydraulic oils tailored specifically to sub-Saharan tropical environments, dust loads, and client machinery parameters.
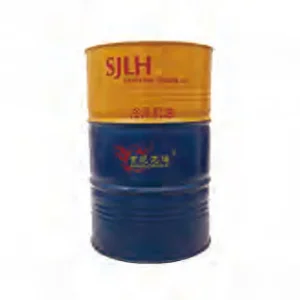
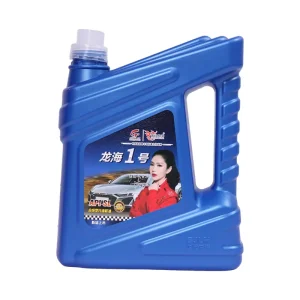
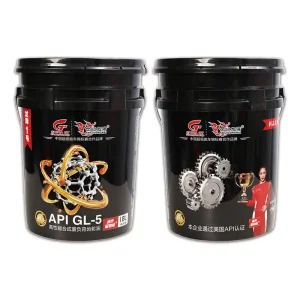
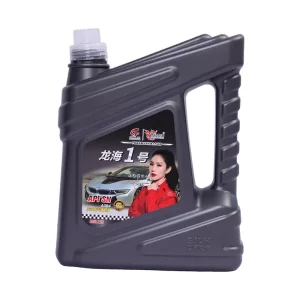
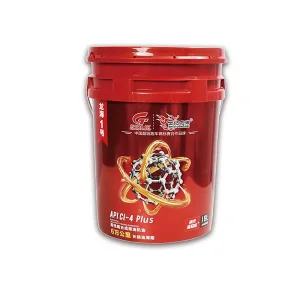
Flexible options ranging from 1L, 4L, and 18L plastic pails to 200L heavy-gauge steel export drums and 1000L IBC totes designed for long sea-freight transit.
Every export batch undergoes spectrometer testing, kinematic viscosity verification, and flash point checking, supported by full ISO 9001 laboratory COA documentation.
Optimized maritime shipment to Port of Nacala or Beira (Mozambique), seamlessly linked with overland bonded transport directly to Chipata, Zambia.
Share equipment specs & volume needs.
Lab analysis & sample sign-off.
Blending & 1‰ precision filling.
Customs clearance & direct shipping.
Expert answers addressing ISO viscosity grades, local climate challenges, fluid maintenance, and import compliance.
Explore our complete range of certified diesel, gear, turbine, and high-efficiency industrial fluids.
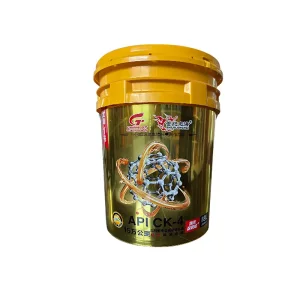
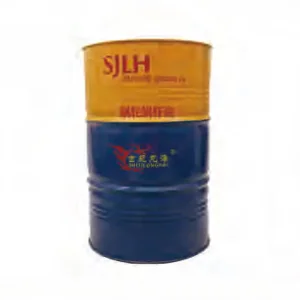
Optimize machinery service life, cut downtime, and secure direct-factory wholesale pricing backed by ISO-certified quality assurance and PICC insurance coverage.
 Longhai